
Share


Dimensional Tolerances in Industrial Magnets: How They Affect the Manufacturing Process
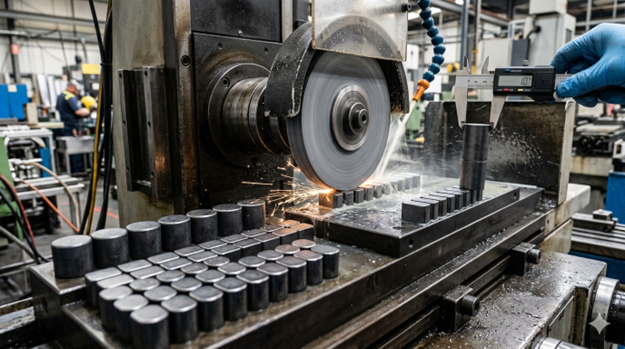
In the field of mechatronic engineering and energy conversion systems, the tolerances of industrial magnets are a critical factor that goes far beyond the simple geometric dimensions specified on an engineering drawing.
Dimensional tolerances in permanent magnets are a direct consequence of the selected manufacturing process and have a decisive impact on assembly, magnetic performance and the final cost of the component. The ability to precisely control the dimensions of permanent magnets during production is therefore fundamental to ensuring reliability and consistency across industrial applications. Understanding how the manufacturing technology determines the achievable tolerances is the first step toward defining the correct specifications for an industrial magnet and avoiding costly design errors during mass production.
In this article, we examine the relationship between the manufacturing process, achievable tolerances and their impact on the final application, as well as the role of quality control and magnetic product development services throughout prototyping and serial production.
Every application has its own specific requirements. To evaluate materials, tolerances and the most suitable design solutions, you can contact our technical team directly.
Why Dimensional Tolerances Are Critical in Permanent Magnets
For industrial magnetic components, dimensions are not merely a mechanical concern. There is a direct relationship between the physical volume occupied by the magnetic material and the behavior of the magnetic circuit in which it operates. A variation of just a few hundredths of a millimeter in a magnet installed inside a rotor or an actuator results in measurable changes to the magnetic field across the air gap, ultimately affecting the performance of the entire application.
For this reason, magnet tolerances must be evaluated from three distinct yet closely related perspectives.
Mechanical Impact
Magnets are frequently bonded or press-fitted onto rotors, stators, ferromagnetic back irons or dedicated housings. Out-of-specification tolerances can lead to incorrect assembly clearances, bonding issues, excessive mechanical stresses during installation and an increased risk of magnet fracture.
Advanced magnetic materials, particularly rare-earth magnets, are inherently brittle and exhibit mechanical behavior similar to that of technical ceramics. This means that insufficient assembly clearance—or localized pressure peaks caused by flatness defects—can initiate catastrophic cracks during press-fitting or axial insertion operations.
For arc-shaped magnets used in brushless motors or Permanent Magnet Synchronous Motors (PMSMs), even slight deviations in curvature or angular geometry alter the contact with the rotor. If the inner radius of the arc magnet does not perfectly match the outer radius of the ferromagnetic rotor core, the adhesive layer becomes uneven.
An excessively thick adhesive layer reduces thermal conductivity, causing the magnet to operate at higher temperatures while weakening its mechanical retention under centrifugal forces. Conversely, an excessively thin adhesive layer may allow direct metal-to-magnet contact, damaging the protective anti-corrosion coating.
Magnetic Impact
From the perspective of magnetics, the dimension of the magnet along the magnetization direction determines its operating point on the BH demagnetization curve. Dimensional variations directly affect the useful magnetic flux across the air gap, the orientation of the magnetic field and the symmetry of the magnetic circuit.
A reduction in magnet thickness caused by a negative dimensional tolerance shifts the operating point toward lower residual induction (B) values. In motors and sensors, this results in cogging torque, torque ripple, positioning errors and reduced repeatability.
When magnets mounted on the same rotor exhibit different thicknesses due to coarse manufacturing tolerances, the resulting asymmetric magnetic imbalance generates Unbalanced Magnetic Pull (UMP). This produces harmful vibrations, acoustic noise and accelerated bearing wear.
Economic Impact
Tighter tolerances inevitably increase the unit cost because they require longer grinding operations, reduce manufacturing yields and demand more accurate measuring equipment. Post-sintering machining of permanent magnets is performed through abrasive grinding, an inherently expensive manufacturing process.
The golden rule of industrial design is to standardize dimensions and specify tight tolerances only where they are functionally required.
Requesting a tolerance of ±0.02 mm where ±0.10 mm would still guarantee the correct performance of the application is one of the most common causes of unnecessary manufacturing costs in mechatronic projects.
The Challenge of Sintering: Anisotropic Shrinkage
To understand where dimensional tolerance limits come from, it is essential to examine the manufacturing process of sintered permanent magnets, the dominant technology for NdFeB and SmCo magnets. The standard production cycle starts with fine magnetic powder and ends with the finished magnet through five main stages: magnetic field pressing, sintering, heat treatment, grinding, and magnetization. Each of these processes introduces specific geometric and dimensional tolerances that accumulate in the final component.
Magnetic Field Pressing
The magnetic powder is compacted inside a die while an external magnetic field aligns the particles along the preferred magnetization direction. This step is what makes the magnet anisotropic: the material is already “programmed” with the direction in which it will later be magnetized.
The density of the green body (the compacted but unsintered part) is not perfectly uniform, since internal powder friction and contact with the die walls create localized pressure gradients.
Sintering and Anisotropic Shrinkage
The green compact is then heated in a furnace to temperatures of approximately 1,000–1,100°C, where the powder particles bond together, densifying the material.
During this stage, the component undergoes significant shrinkage and, more importantly, anisotropic shrinkage: the contraction along the magnetization direction differs from that in the perpendicular directions.
For sintered NdFeB magnets, shrinkage along the magnetization axis is typically 15–25%, while shrinkage in the transverse directions ranges from 5–15%.
As a result, the tooling must be designed using three different scaling factors, and the sintered magnet still leaves the furnace with dimensional tolerances typically around ±0.1 / ±0.2 mm.
Moreover, anisotropic shrinkage does not only produce linear dimensional variations. It often causes geometrical distortions, such as waist-shaped deformation (“hourglass effect”) or warping of flat surfaces, making the raw component unsuitable for direct mechanical assembly without secondary machining.
Grinding
To achieve tight dimensional tolerances, the sintered magnet must be precision-ground using diamond grinding wheels or dedicated CNC grinding machines.
Grinding provides the flatness and parallelism required for assembly while producing the surface finish needed for adhesive bonding or subsequent coating processes.
It is, however, a slow and expensive operation. Rare-earth sintered magnets are extremely hard and brittle, grinding wheels wear rapidly, and material removal rates are necessarily limited.
The Alternative: Injection and Compression Molding
Not all permanent magnets require sintering followed by precision grinding.
Bonded magnets offer a fundamentally different manufacturing approach and are particularly advantageous for components with highly complex geometries.
Unlike sintered magnets, bonded magnets consist of magnetic particles dispersed within a polymeric matrix, such as PA6, PA12, or epoxy resin.
Because of this manufacturing method, bonded magnets do not experience the severe anisotropic shrinkage associated with sintering. Instead, they accurately reproduce the mold geometry, with injection molding shrinkage remaining isotropic and highly predictable, depending primarily on the volumetric properties of the thermoplastic polymer.
Their greatest competitive advantage lies in the ability to integrate complex geometries into a single molded component, eliminating assemblies that would otherwise require multiple precision-ground sintered parts. This completely removes the costs and lead times associated with secondary grinding operations.
Although the overall magnetic properties—such as Br and (BH)max—are lower than those of fully sintered magnets due to the presence of the polymer binder, the intrinsic dimensional accuracy of the molding process eliminates the need for post-molding mechanical machining.
Comparative Analysis: Typical Dimensional Tolerances by Magnet Family
Dimensional tolerances cannot be specified independently of the manufacturing process. Each magnet family follows a specific production route that ultimately determines the level of dimensional precision that can realistically be achieved.
| Technology / Material | Standard Tolerance (As-Sintered / As-Molded) | With Precision Grinding | Key Notes |
|---|---|---|---|
| Sintered NdFeB | ±0.1 / ±0.2 mm | Up to ±0.02 mm | Precision grinding is almost always required for tight mechanical fits. |
| Sintered SmCo | ±0.1 / ±0.2 mm | ±0.05 mm | Extremely brittle; machining may cause microcracks. |
| Sintered Ferrite | ±0.1 / ±0.2 mm | ±0.1 / ±0.2 mm | Precision grinding is generally reserved for specialized applications. |
| Injection-Molded NdFeB / Ferrite | ±0.5 mm | Not required | Mold precision enables complex geometries without secondary machining. |
| Compression-Bonded NdFeB | ±0.1 mm | Not required | High dimensional accuracy directly from the molding process. |
Quality Control and Tolerance Validation
Specifying dimensional tolerances on a technical drawing is only half the job. Ensuring that every production batch consistently meets those specifications requires a structured and repeatable quality control system, especially in high-volume manufacturing.
For permanent magnets, dimensional inspection is just as important as magnetic testing. A magnet that meets dimensional specifications but falls outside the required Br or Hc values is just as non-compliant as a magnet with correct magnetic properties but incorrect dimensions.
Typical equipment used during our quality control process includes Coordinate Measuring Machines (CMMs) for complex geometries and GD&T (Geometric Dimensioning and Tolerancing) verification, including flatness, parallelism, perpendicularity, and concentricity measurements on ring magnets and arc-shaped magnets.
One of our key strengths is the use of identical metrology equipment across all business units, ensuring consistent measurement methods and uniform product performance for every customer.
Project Development: Optimizing the Value Chain
Dimensional tolerances in permanent magnets represent the point where design specifications, manufacturing processes, and quality control converge.
They are not arbitrary values added to a drawing but the direct result of a well-defined industrial process. Understanding this manufacturing chain is essential for defining realistic specifications, selecting the most appropriate production method, and optimizing component cost.
The real added value within the supply chain lies in providing advanced engineering support, from initial material selection through final metrological validation. This is what differentiates a catalogue supplier from a true engineering partner.
Our engineering team can support projects from the earliest prototyping stages by:
- Optimizing component dimensions based on the expected anisotropic shrinkage, minimizing the amount of stock material that must be removed during grinding.
- Recommending chamfers and edge radii to significantly reduce chipping during transportation and automated assembly operations.
- Balancing mechanical assembly tolerances with the magnetic tolerances defined by the BH curve, ensuring maximum magnetic flux stability within the air gap while avoiding unnecessary manufacturing costs.
Our ability to support every stage of the development process allows us to deliver highly accurate magnetic solutions tailored to the specific requirements of each industrial application.
Working with Tight Tolerances or Complex Geometries?
Contact our engineering team for a technical evaluation of your design specifications and to identify the manufacturing process best suited to your magnetic component.


